Pristine Chemicals

About us

Quality, innovation, and long-term supply partnerships

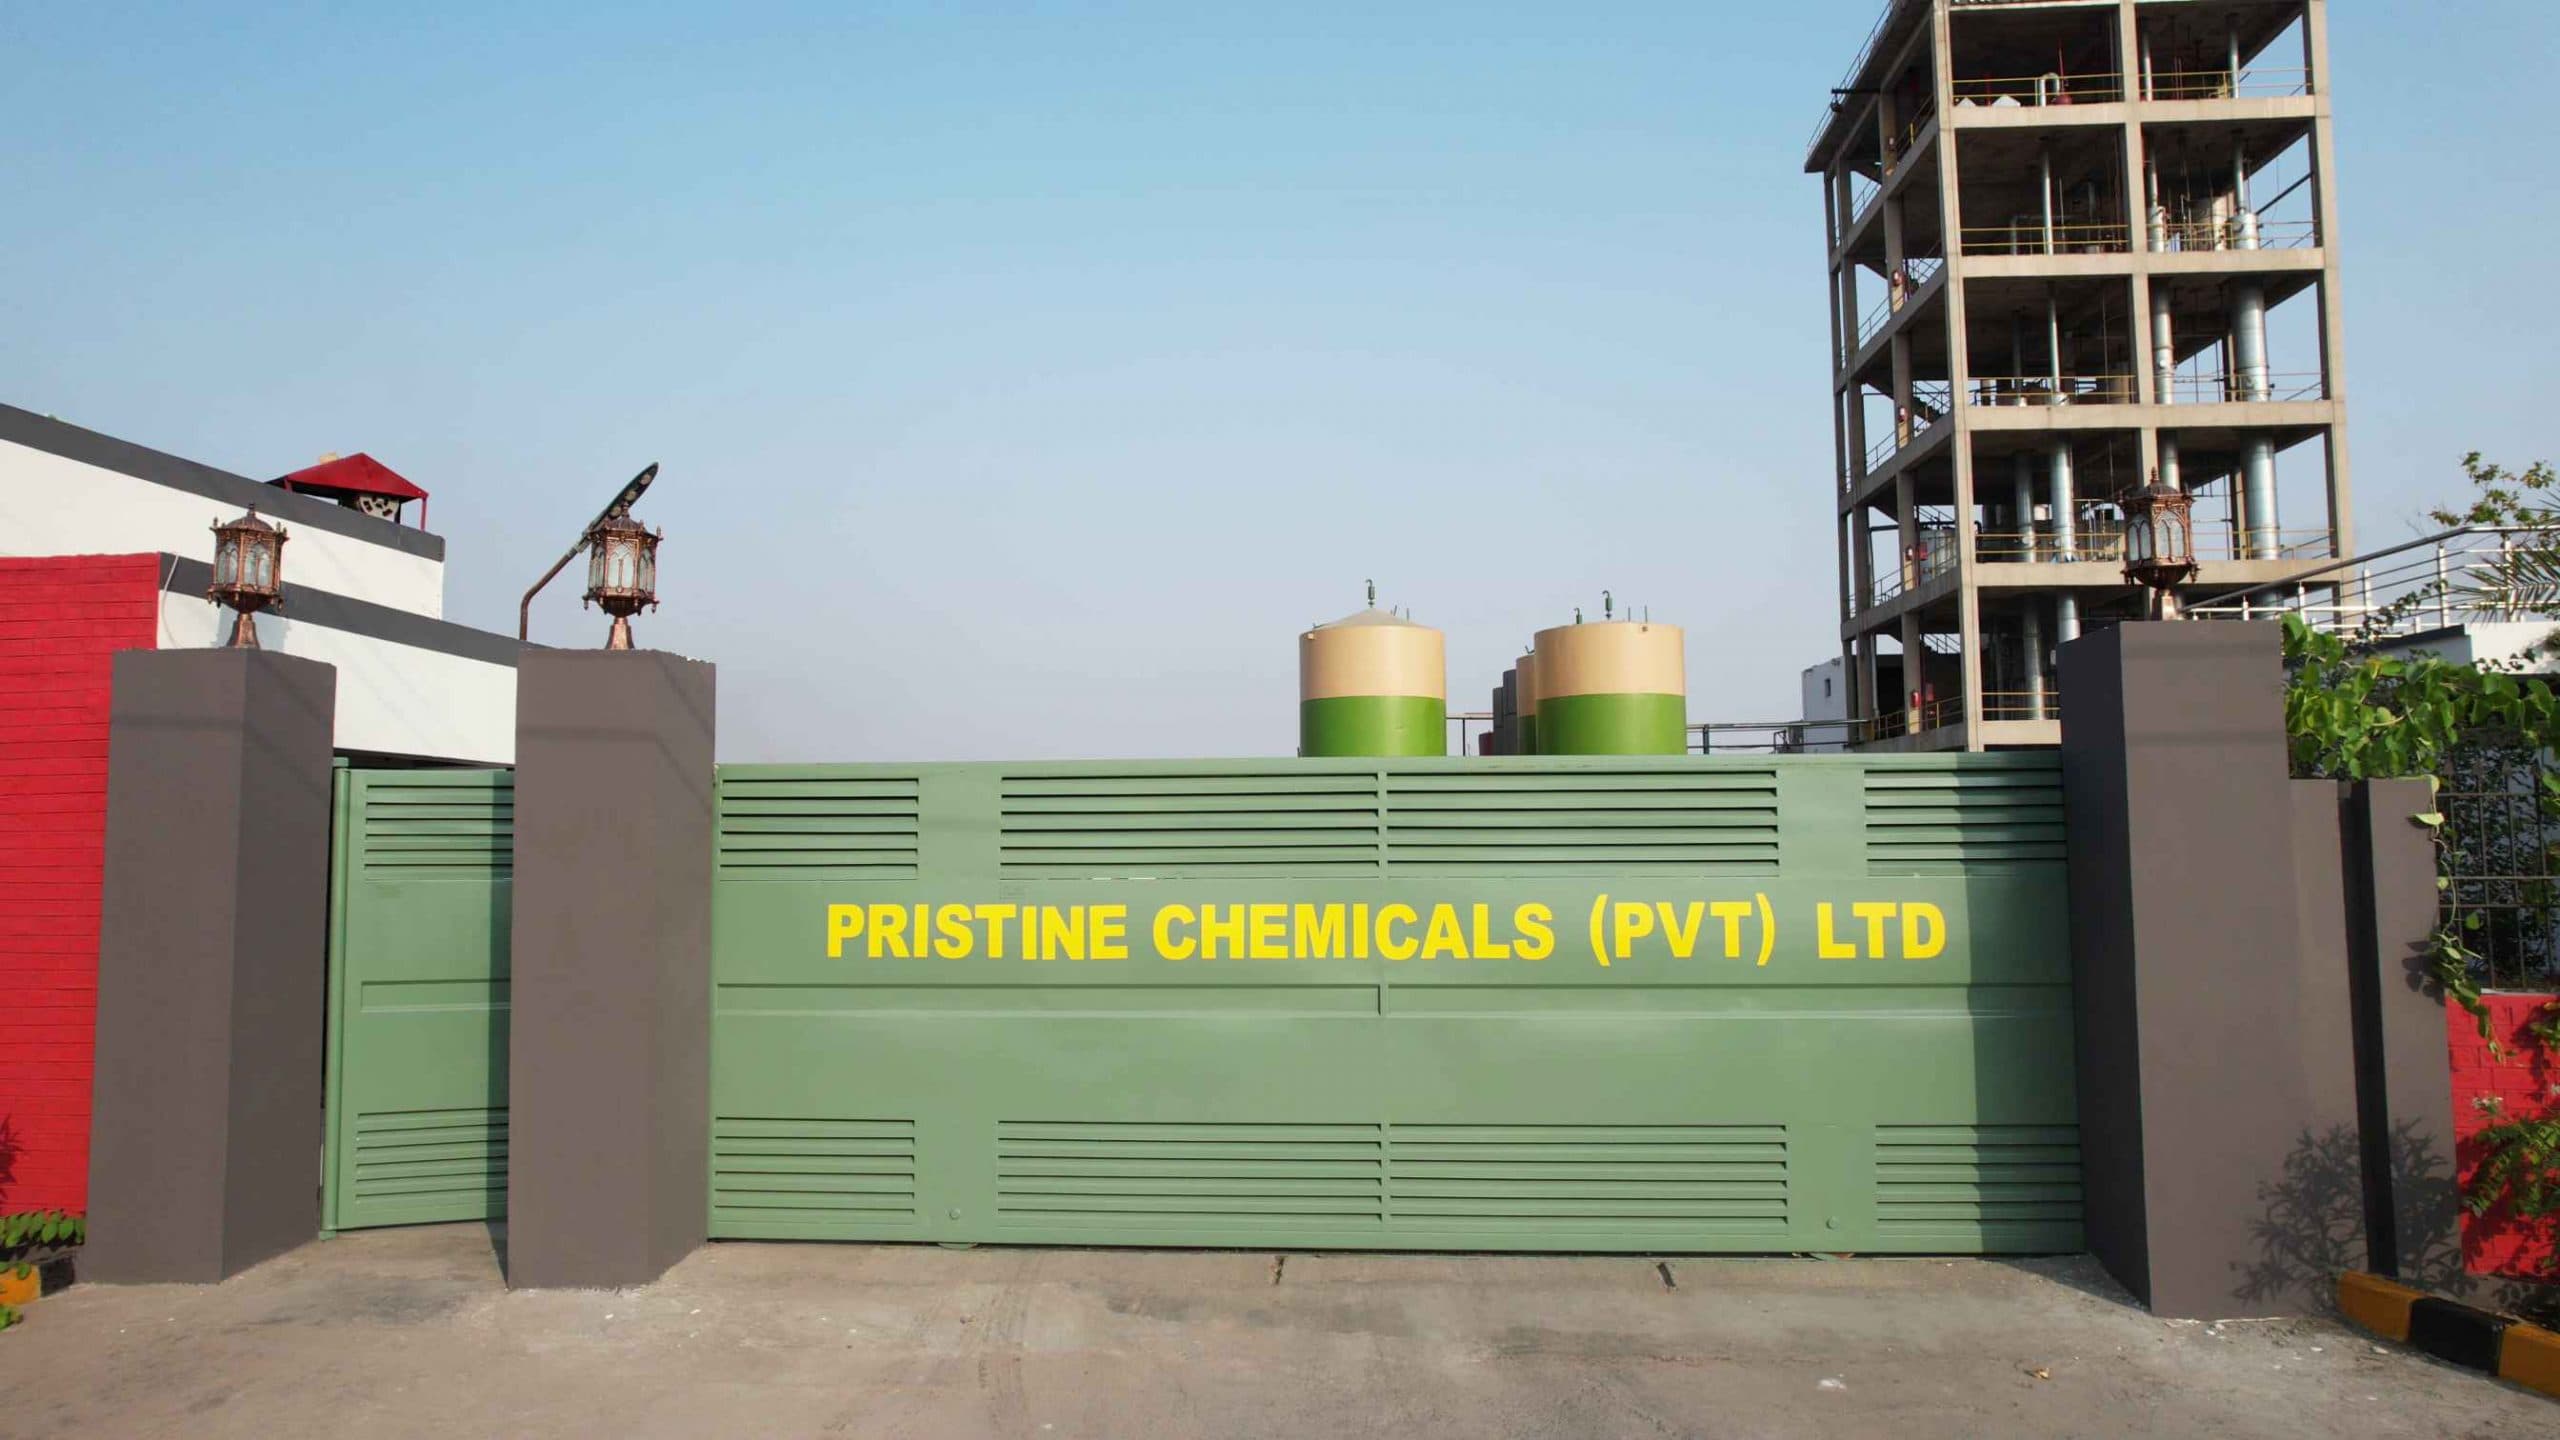
Pristine Chemicals Pvt. Ltd. is located in Vehari Industrial Estate, Punjab, Pakistan. The Pristine Chemicals group stands among the most recognized chemical producers in Pakistan through a relentless drive for international quality standards.

Pristine Chemicals Pakistan

Pristine Chemicals Group of Industries Pakistan

Pristine Chemicals Group of Industries Pakistan

Pristine Chemicals is an ISO 9001:2015 (Quality Management System) and ISO 14001:2015 (Environmental Management System) certified group incorporated in Pakistan under the Companies Ordinance 1984, governed by the regulations of the Securities & Exchange Commission of Pakistan.

The group includes Pristine Chemicals, Pristine Chemicals Pakistan, Pristine I.Chem Solution, Pristine Diagnostics, and Pristine Chemicals Pvt. Ltd. — producing ethyl acetate, butyl acetate, methyl acetate, isopropyl alcohol, NPA, NPAC, Unisol, xylene, pigments, lacquers, adhesives, and printing inks.

Pristine Chemicals Group of Industries stands proudly among the most recognized chemical producers in Pakistan through a relentless drive to achieve international quality standards.

“We firmly believe that customer satisfaction is the number one factor behind our success.”

ISO 9001:2015ISO 14001:2015SECP RegisteredEst. 2017
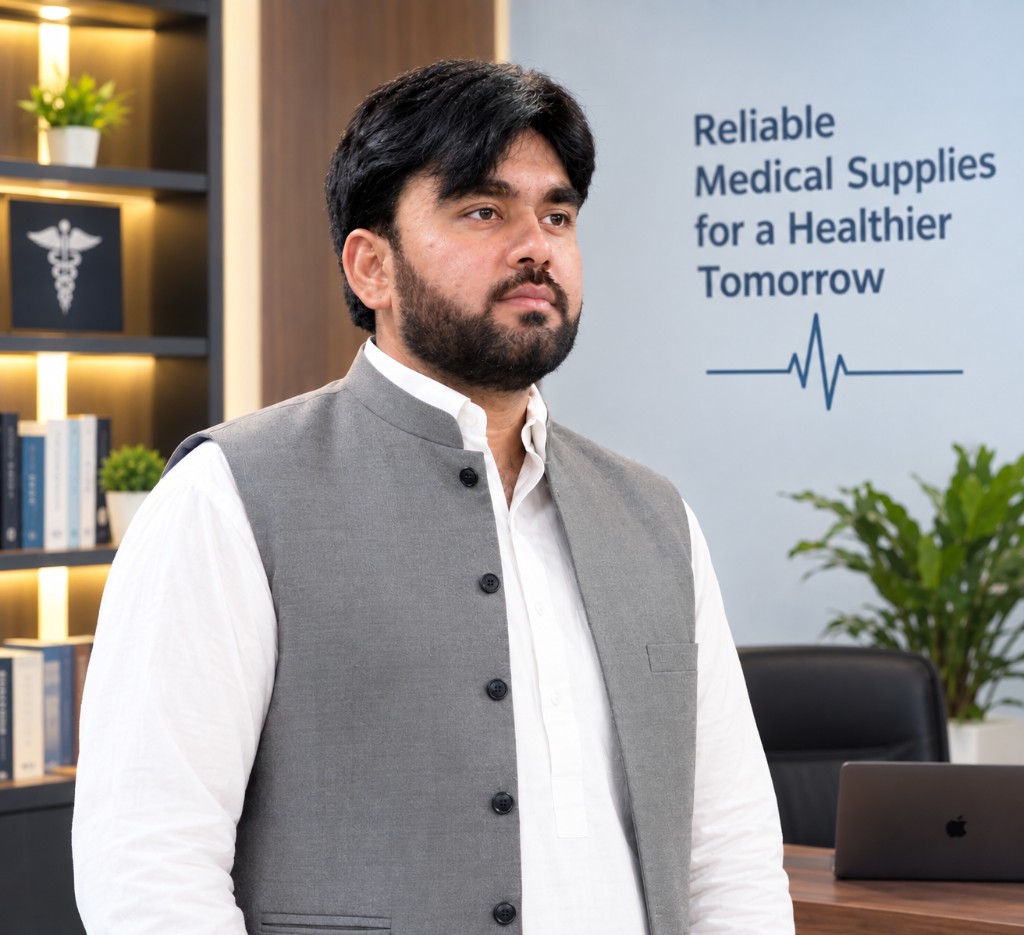
Rao M. Faisal Taufiq

CEO's message

Rao M. Faisal Taufiq

CEO, Pristine Group of Chemicals

The economic, environmental, and social implications of business are more important than ever. We build partnerships with our customers through knowledge, ingenuity, and the commitment of our people. Quality control is the driving force behind our success — each batch passes rigorous SOP-based testing with full traceability.
Production & capacity

Total production exceeds 15,000 MT per year. Ethyl acetate runs at ~25 MT/day with purity ≥99.9% and moisture <0.03%; butyl acetate and NPAC average ~10 MT/day each.

Ethyl AcetateButyl AcetateNormal Propyl Acetate (NPAC)Unisol99% Isopropyl Alcohol (IPA)Methyl Acetate
View full product range →

Vision

To be a highly reliable, innovative, and reputable chemical company.

Mission

To satisfy customers by providing quality, innovative, and assorted chemical products that increase productivity while reducing cost.

Values

  • Quality
  • Innovation
  • Health & Safety
  • Continuous Improvement
  • Integrity

Quality assurance & dispatch

Our quality assurance team ensures cleaned, approved drum packing and on-time delivery from a large warehouse stock. Safety measures and continuous improvement are embedded across production, loading, and dispatch.

  • Large warehouse stock for reliable, on-time delivery when you place an order.
  • Products supplied in cleaned, quality-approved drums.
  • Quality Assurance team verifies packing before dispatch.

8+

Core products

25+

Enterprise customers

2

Locations

2

ISO systems

Manufacturing

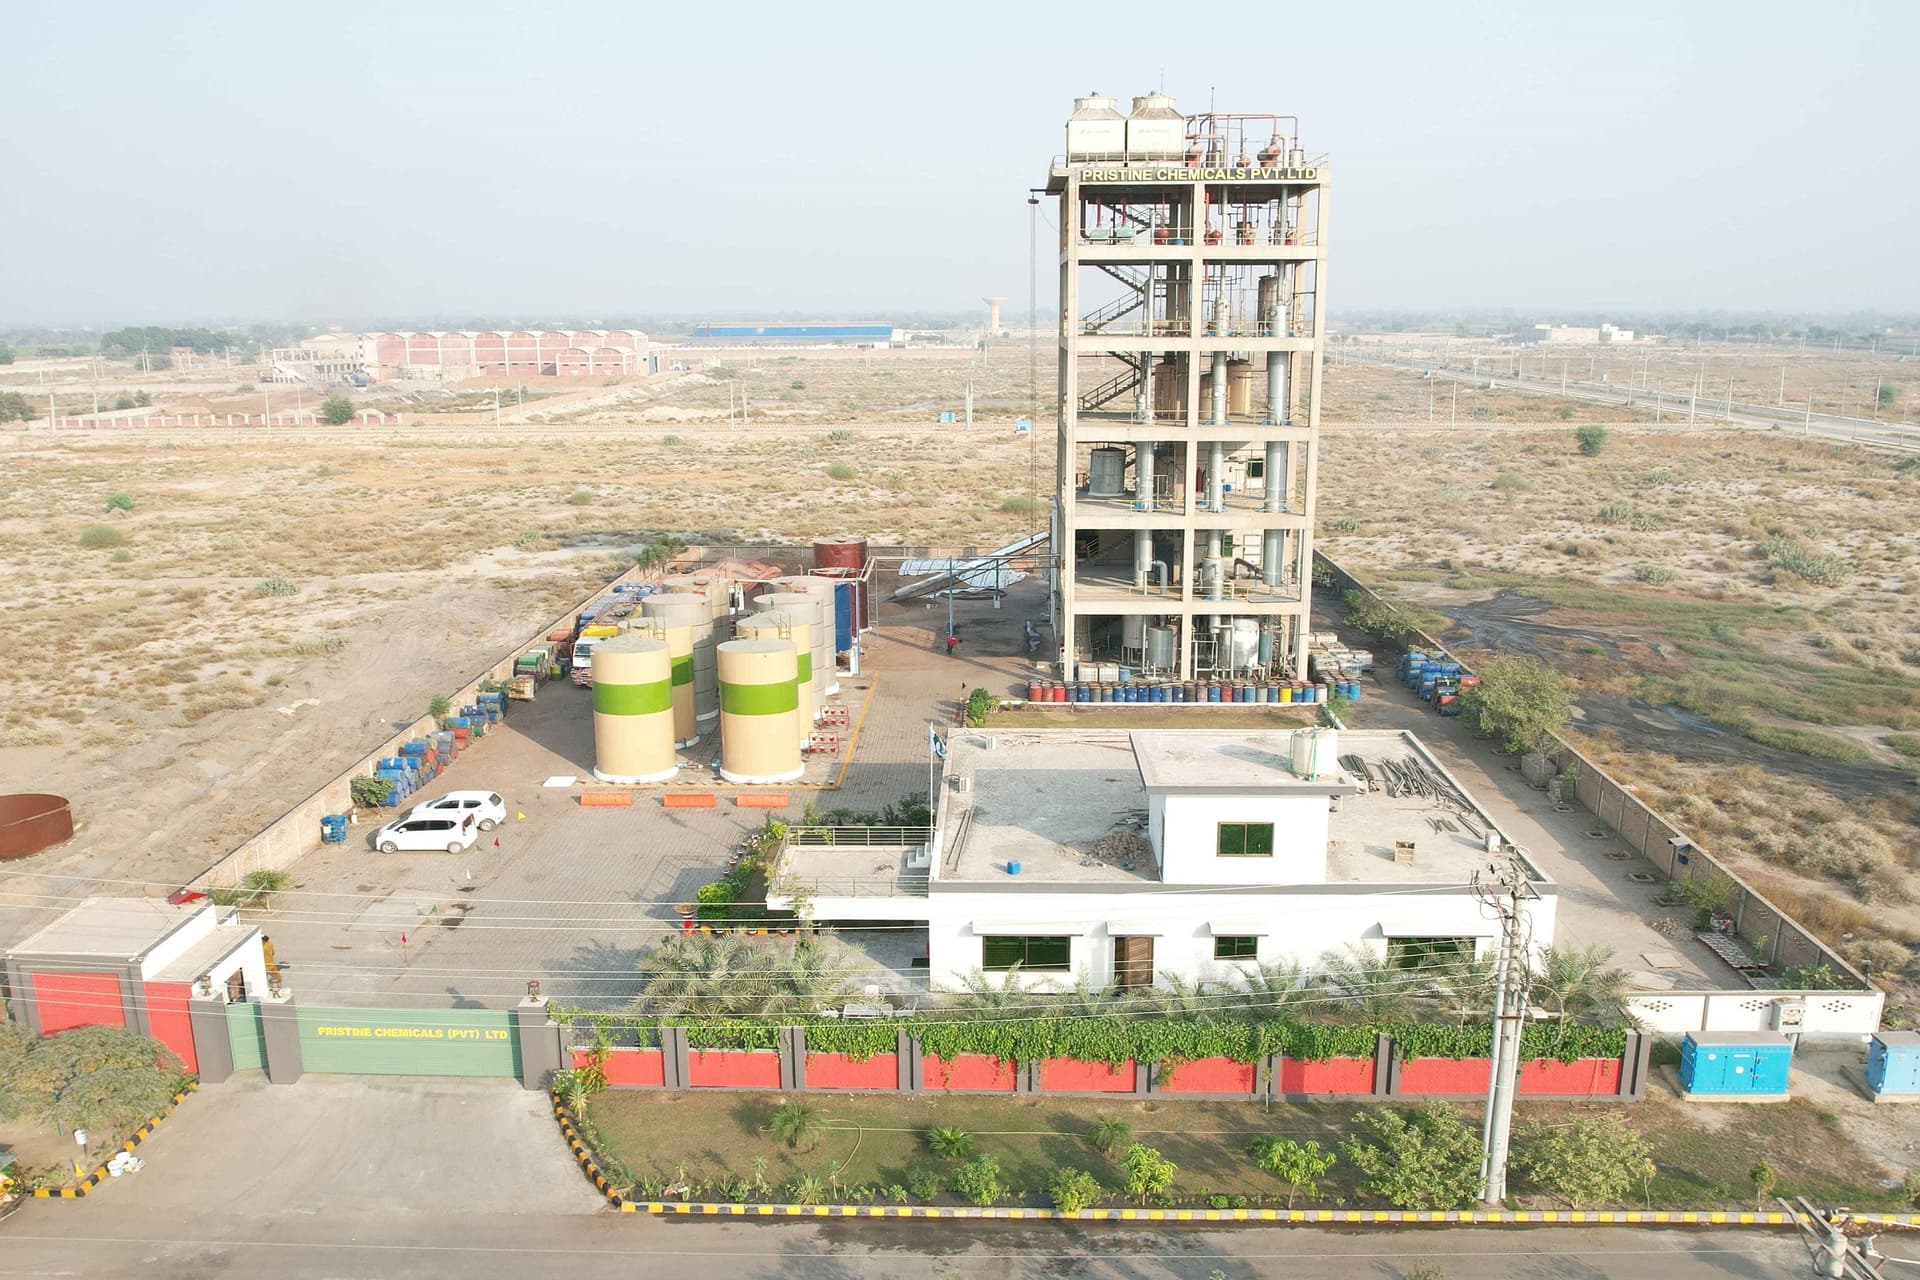
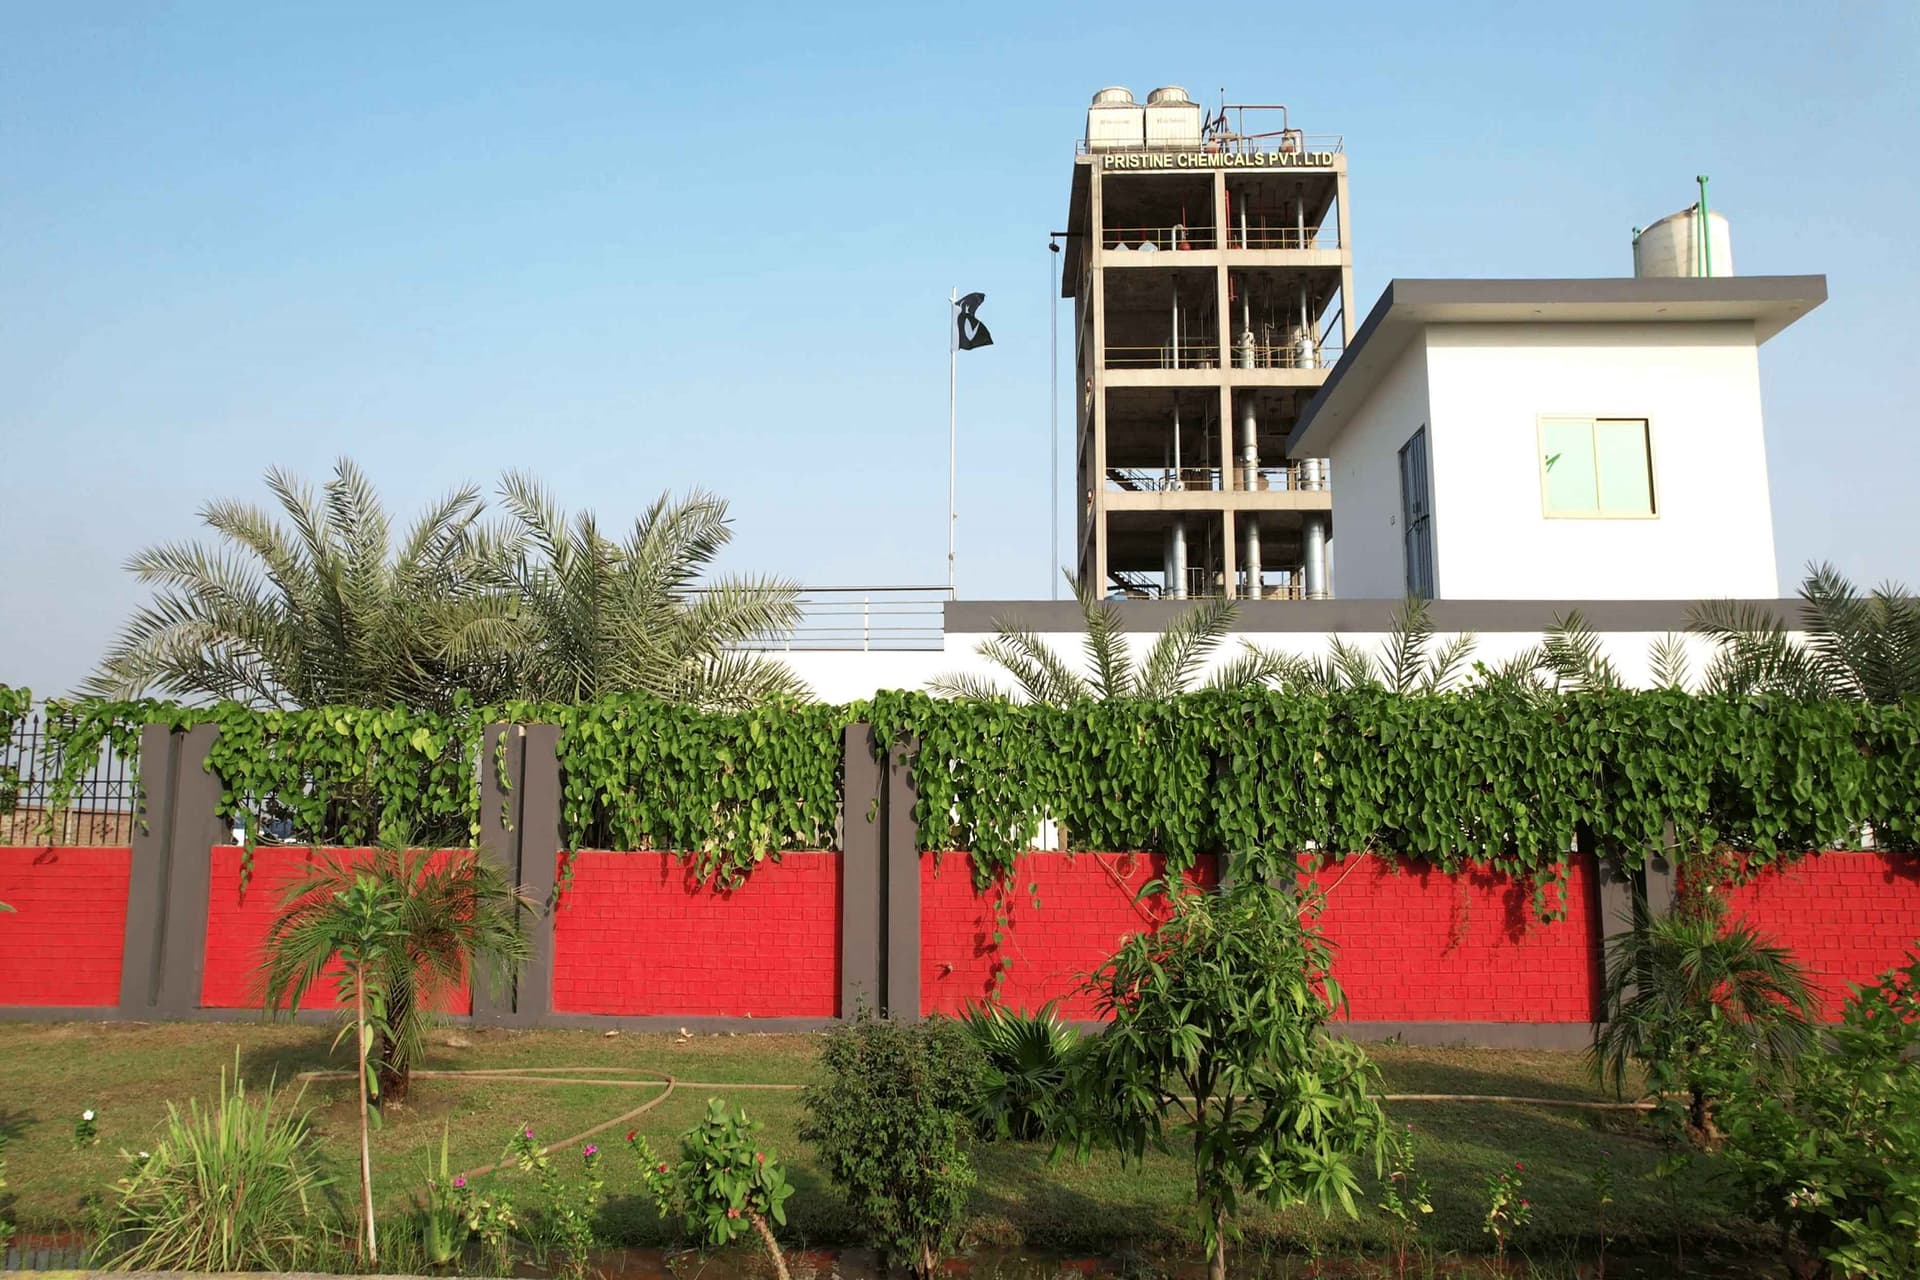
Plant at Vehari

Production, warehouse stock, loading bays, and dispatch from our Vehari Industrial Estate facility.

Full operations →
Overall view of Pristine plant
Front view of plant
Front view of plant
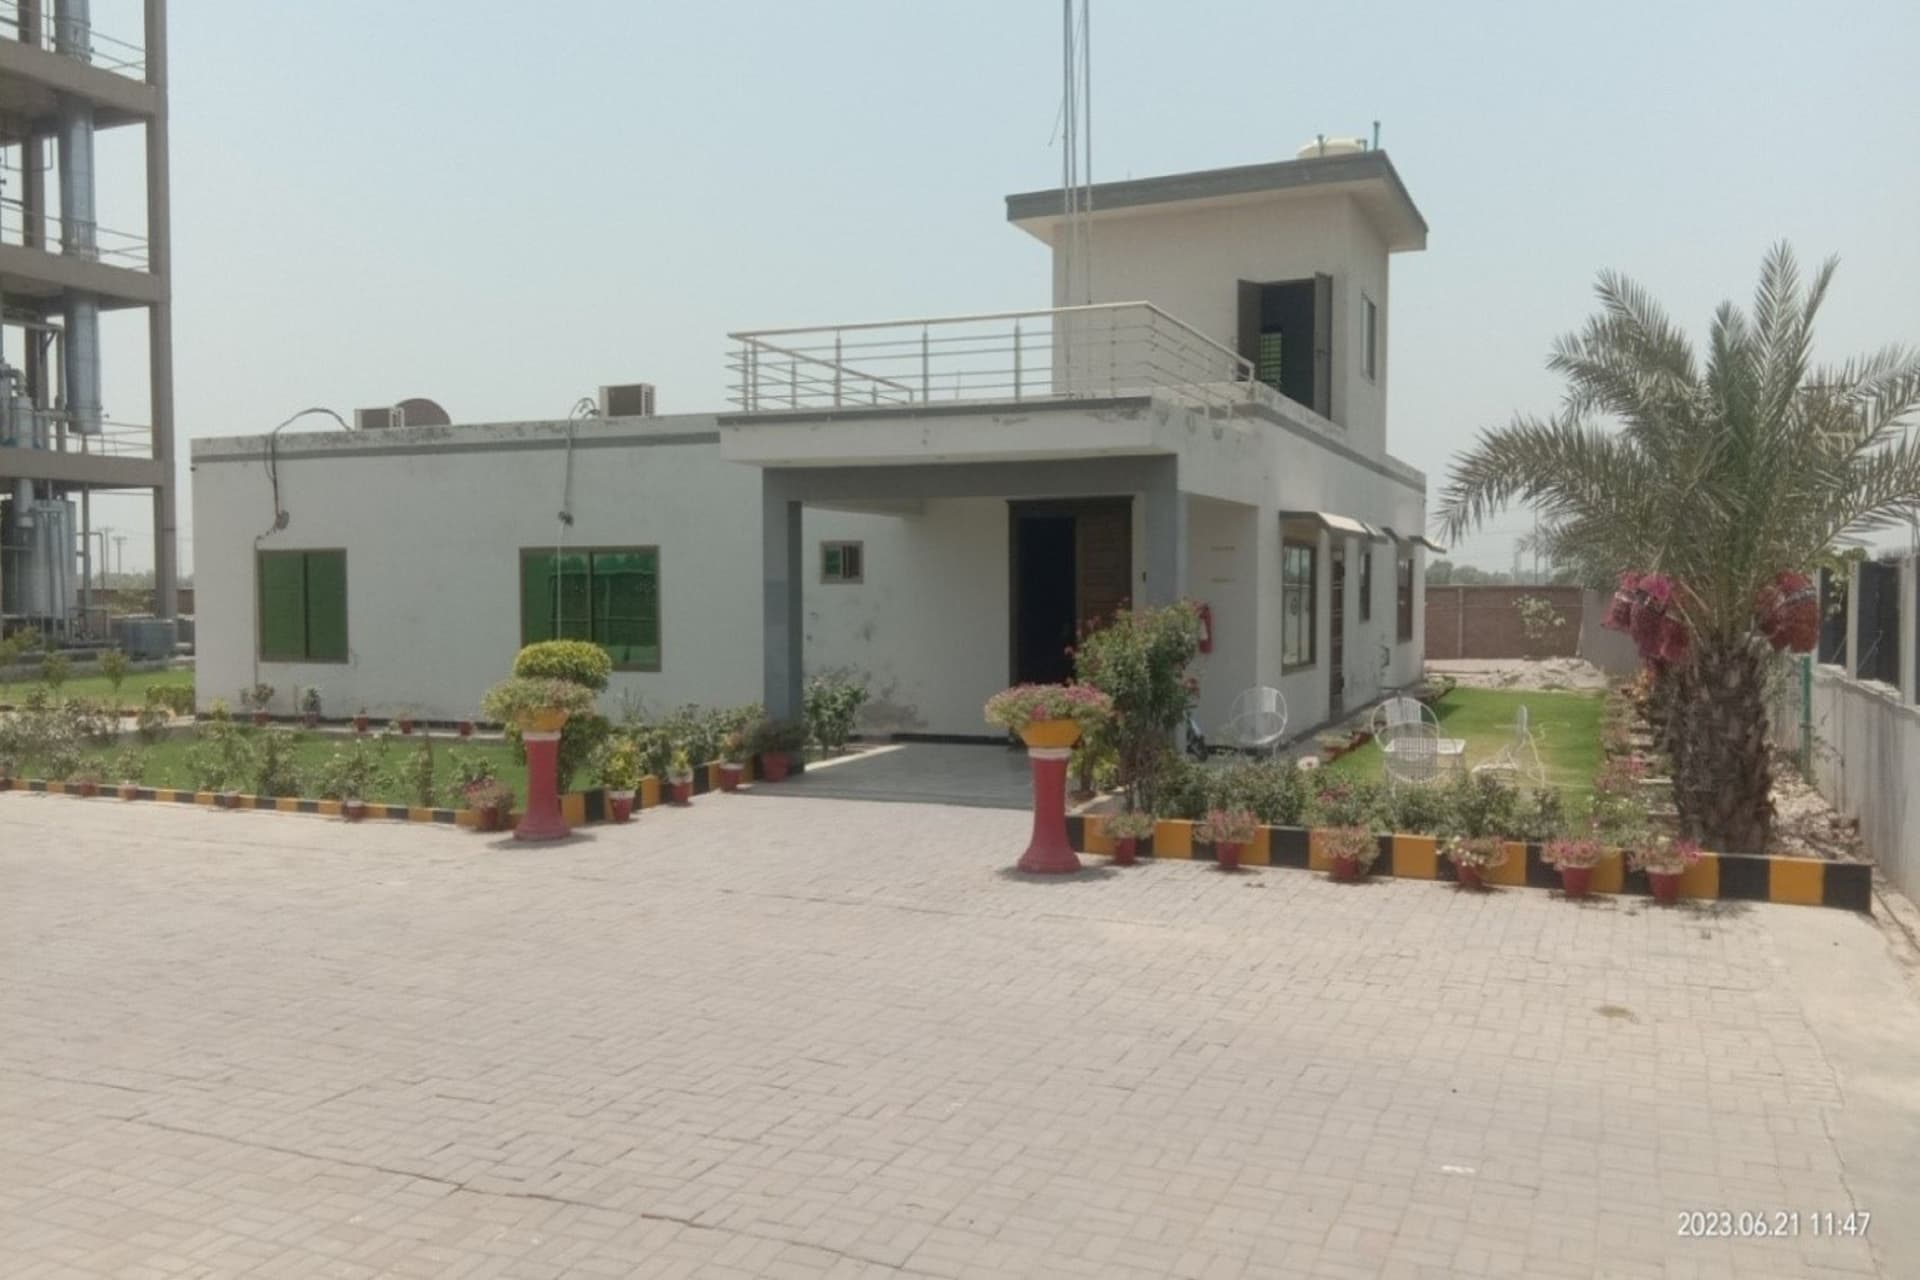
Admin office block
Admin office block

Compliance

Certified management systems

All certificates →
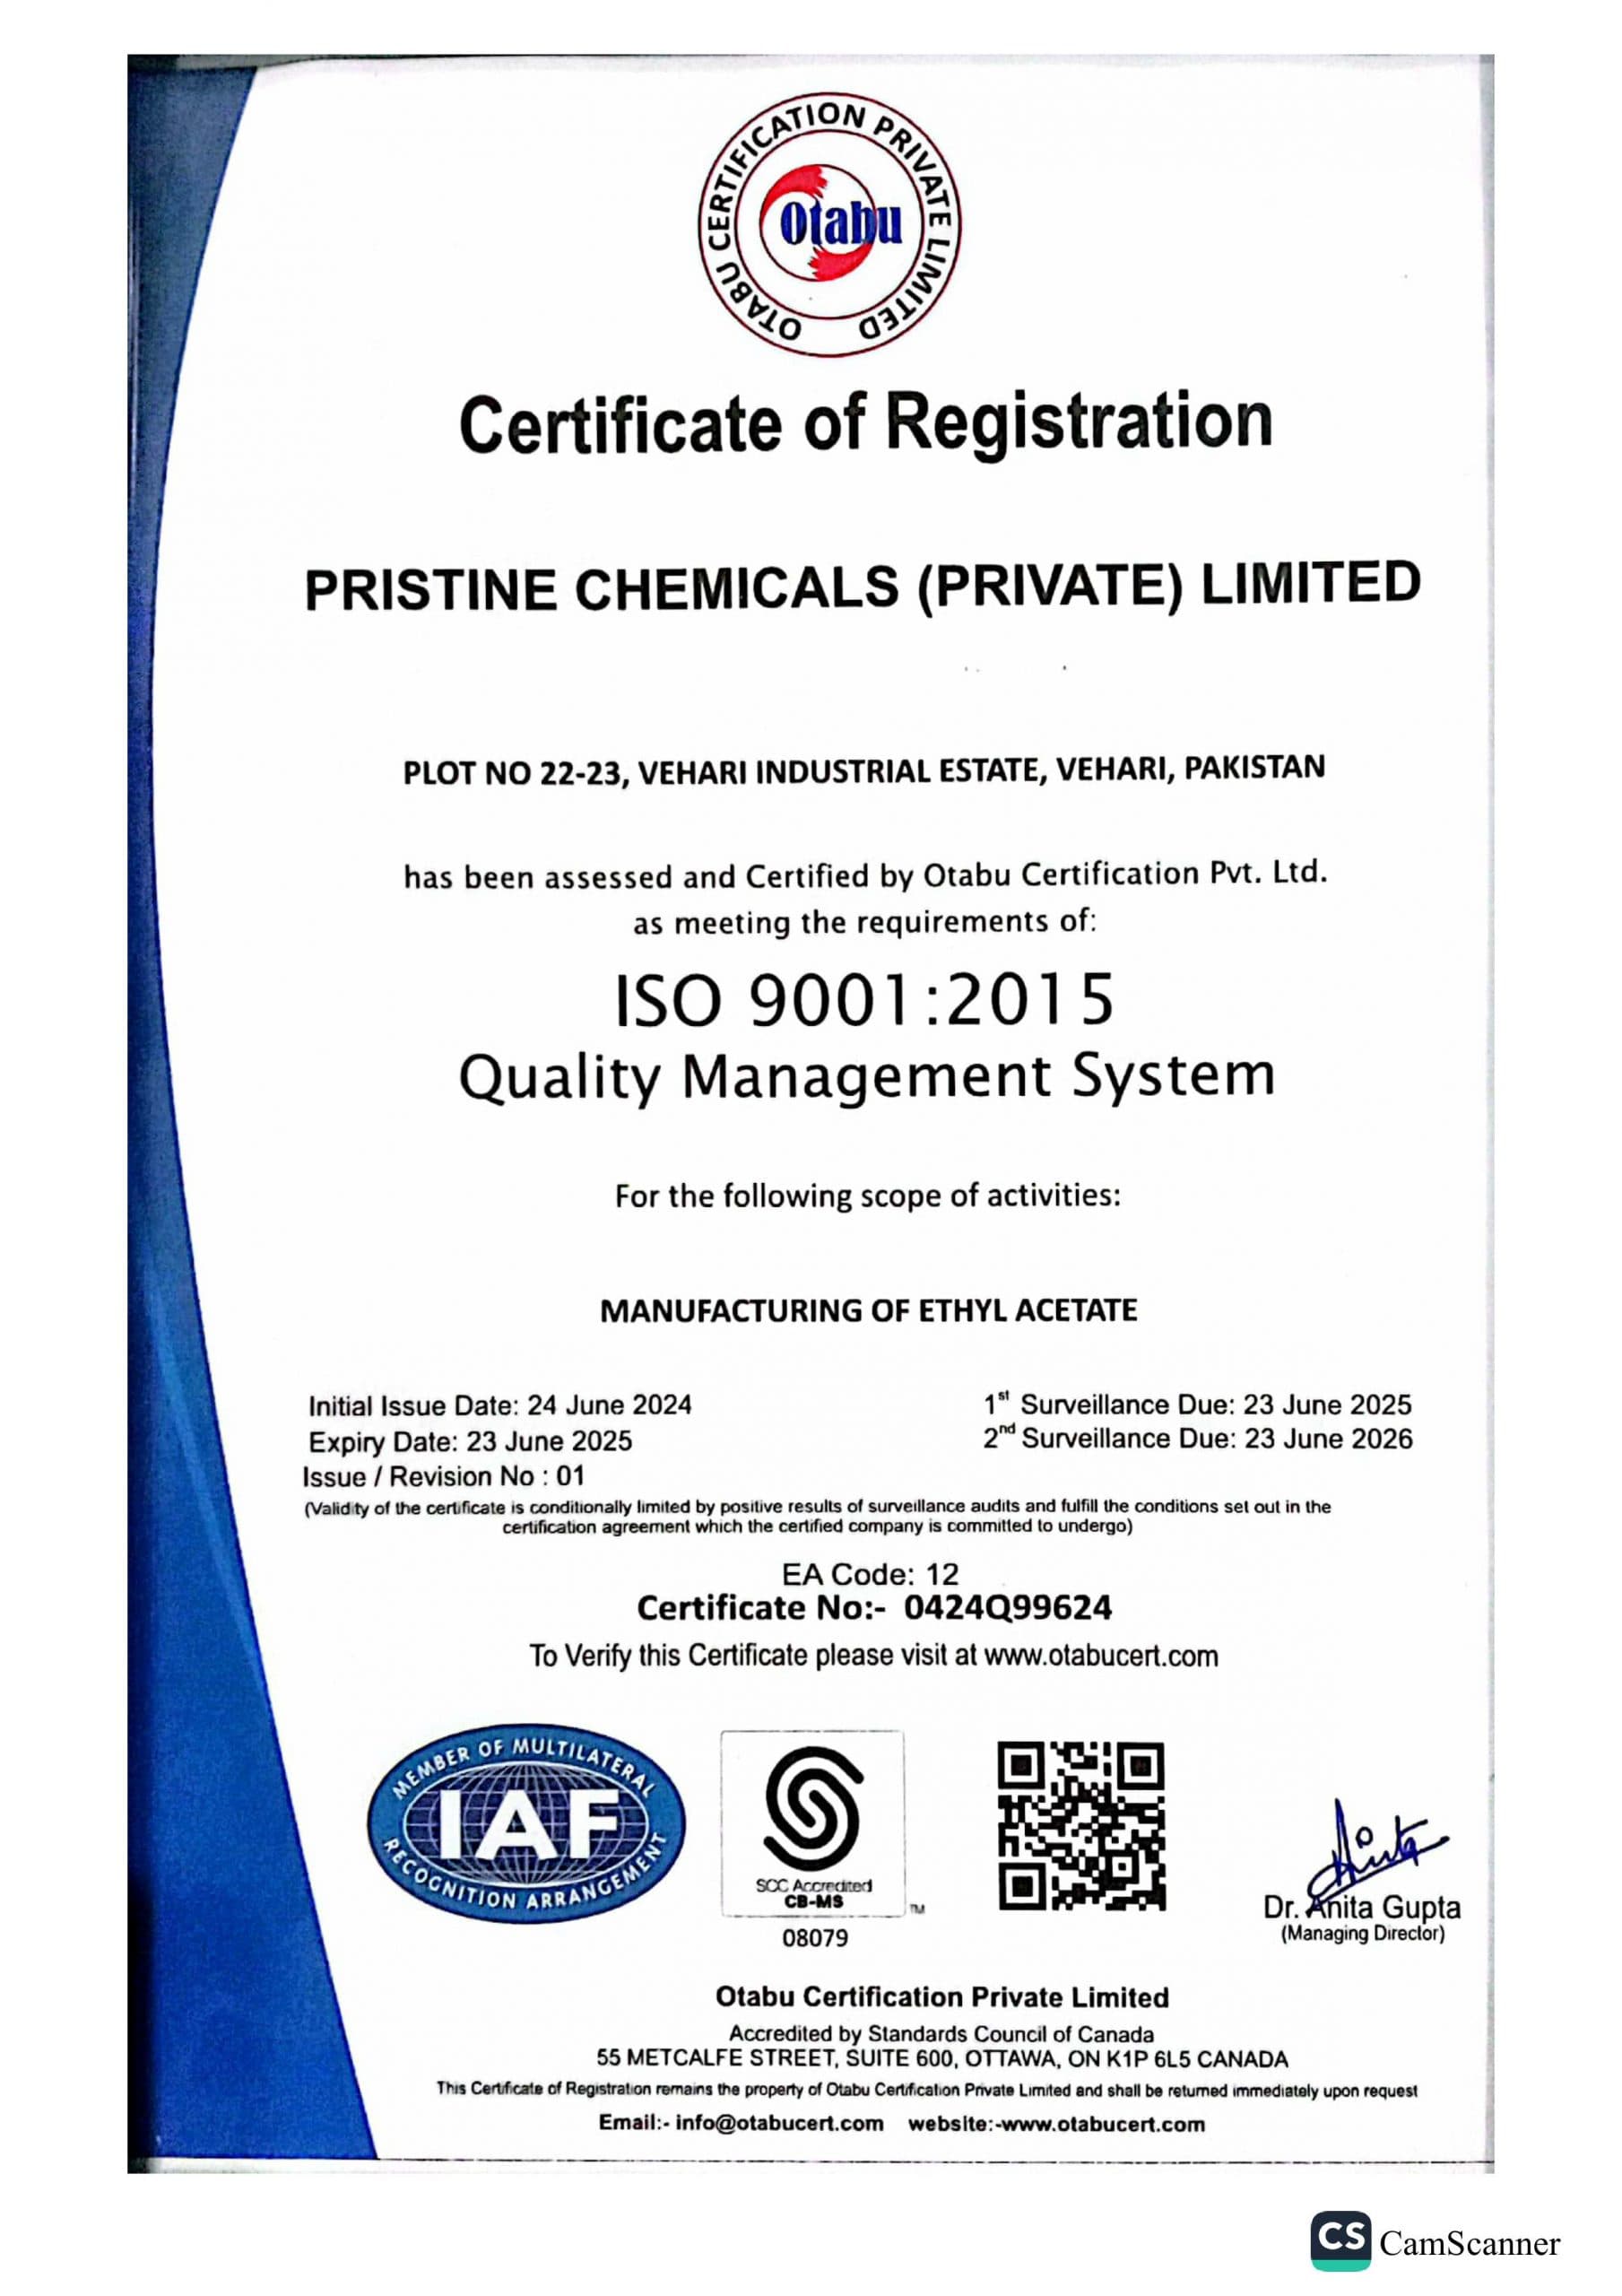
ISO 9001:2015

ISO 9001:2015

Quality Management

Systematic quality management across production, testing, and dispatch.

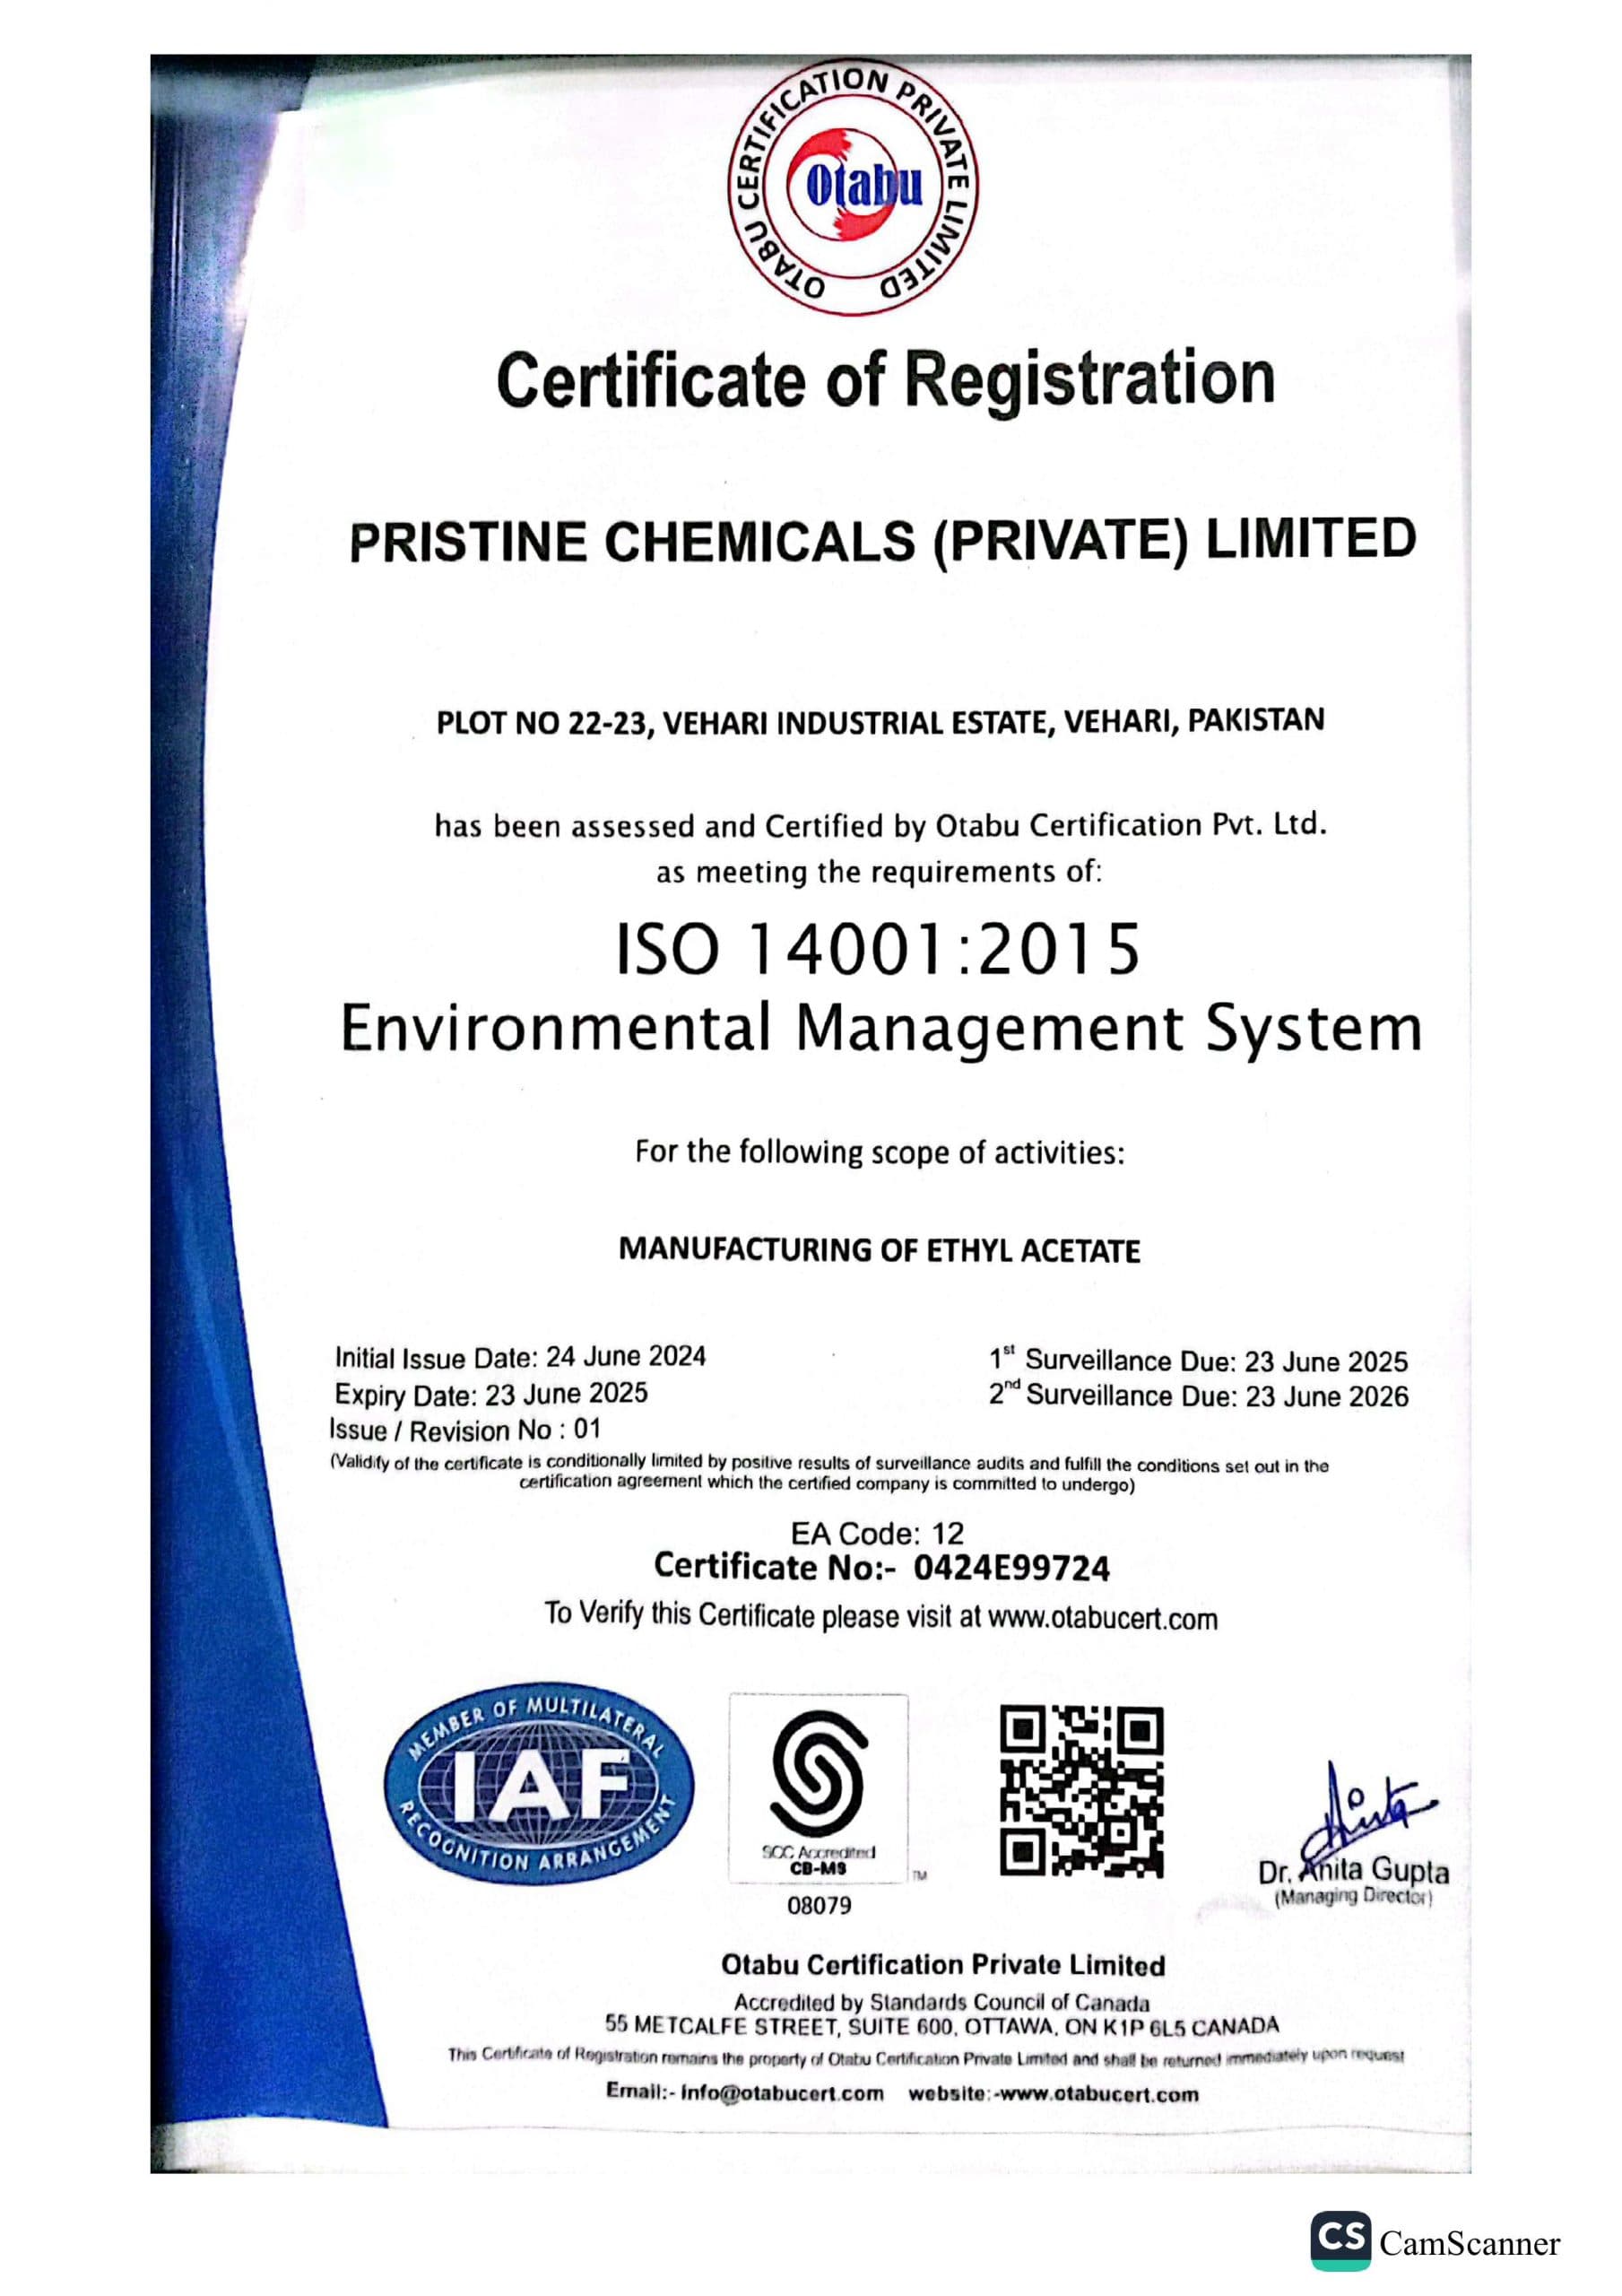
ISO 14001:2015

ISO 14001:2015

Environmental Management

Environmental stewardship integrated with manufacturing operations.

Our team

Leadership, production, QA/QC, and engineering.

Meet the team →

Operations

Plant gallery, packing, and safety measures.

View operations →

Products

Solvents, diluents, and specialty chemicals.

Browse products →

Contact

Quotes, logistics, and technical support.

Get in touch →